
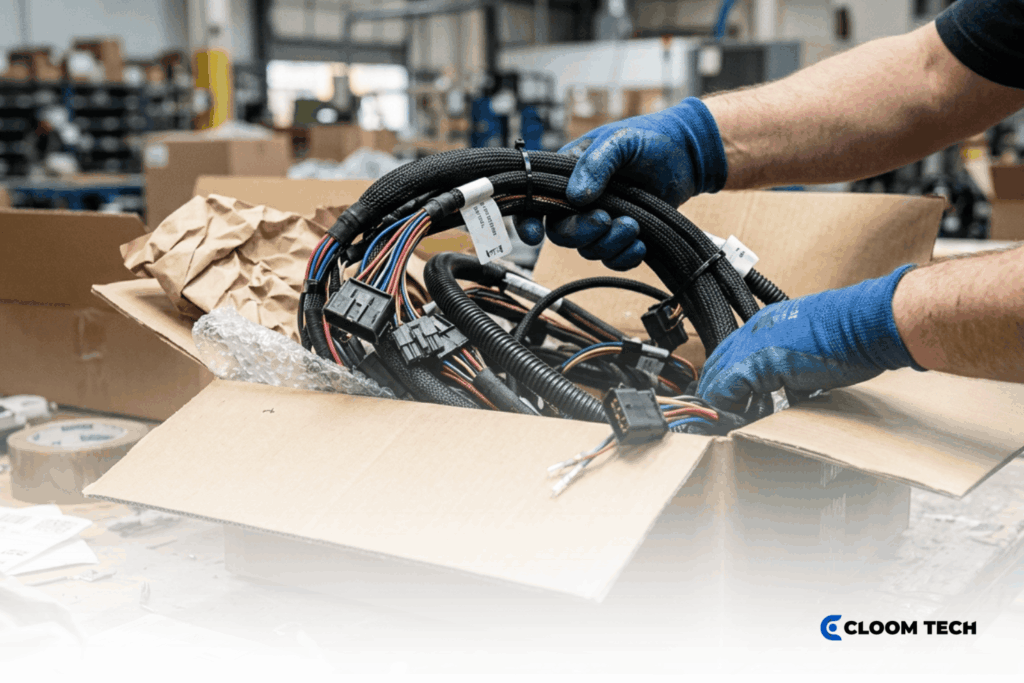
Wire harness quality control (QC) starts before you award a purchase order by confirming how a supplier will verify your assembly requirements. Wire harness inspection records then let you compare the approved sample with your production specification and acceptance criteria.
Start by requesting a sample inspection report with measured branch lengths and crimp pull-force results against specified limits. Then check how the supplier handles failed measurements, including records showing rejected assemblies stayed on hold until reinspection confirmed compliance.
Why Wire Harness Quality Control is a Buyer’s Job Too
A supplier’s QC system can only check a harness against the requirements you give it. If your documents don’t define acceptance criteria, approval authority, and expected evidence, the supplier sets them for you. You then carry the risk when a harness fails in the field.
Therefore, name who approves samples and authorizes exceptions, and make shipment acceptance conditional upon receiving the inspection deliverables specified in your drawings. For offshore sourcing, fix the approved manufacturing site so any factory transfer triggers change-control review. For broader sourcing checks, see our guide to evaluating a Chinese wire harness manufacturer.
Certifications to Verify
ISO 9001 sets quality management requirements for consistently meeting customer requirements through controlled processes. Verify that the certificate covers the manufacturing site and activities your order requires.
For automotive work, IATF 16949 replaced ISO/TS 16949, so confirm the supplier holds a current IATF 16949 certificate.
| Certification | Evidence to Check | Verification Route |
|---|---|---|
| ISO 9001 | Factory address, manufacturing scope, and certificate dates | Confirm with the issuing certification body |
| International Automotive Task Force (IATF) 16949 | Certificate number and production-site identity | Certificate verification guidance |
| ISO 13485, when applicable | Scope covering wiring harness or cable assembly manufacturing | Confirm scope with the issuing body |
Confirm the Workmanship Class
IPC/WHMA-A-620 sets workmanship acceptance criteria for cable and wire harness assemblies. Select the class from your product’s service requirements, then state the agreed revision and class in your purchasing documents.
The product-class definitions describe service expectations, while individual workmanship criteria decide whether a condition is acceptable. While personnel training credentials show individual qualifications, they do not guarantee process capability. Therefore, verify any required manufacturing-process qualifications separately.
| Class | Service Requirements |
|---|---|
| Class 1 | A completed assembly function is the primary requirement |
| Class 2 | Extended service life and continued performance, with uninterrupted service desirable but not mandatory |
| Class 3 | Continued performance or performance on demand where downtime is unacceptable, potentially in harsh environments |
Wire Harness Inspection Checkpoints to Ask About
Request receiving inspection records, crimp setup measurements, and final test reports from the same production lot. Compare the results with your drawing revision and acceptance limits, then confirm how the supplier isolates failed assemblies before reinspection.
Incoming Material Inspection
Our incoming material checks compare wire specifications and component part numbers with your approved bill of materials (BOM). We retain receiving records and material-lot identification for your review.
If terminals differ from the approved BOM, require written substitution approval before the supplier uses that stock.
In-Process Inspection
Before releasing crimping, we verify wire and terminal part numbers against the assigned tooling and application specification. Our setup records include crimp-height measurements and required sample pull results, while your inspection plan controls follow-up checks and crimp cross-sections.
Ask any supplier how it handles these production controls:
- Terminal insertion: How do operators confirm contact seating and locking-feature engagement?
- Inspection frequency: When do operators repeat checks after setup or tooling adjustments?
- Failure response: Which assemblies does the supplier isolate after a measurement fails?
A generic “visual check completed” entry proves little unless the record names the feature checked and the acceptance criteria applied.
First Article Inspection and Sample Approval
First article inspection (FAI) should verify the sample against the released drawing and BOM before you authorize mass production. Review these physical features alongside the electrical and mechanical evidence your approval plan requires:
| Feature | Evidence to Review |
|---|---|
| Branch geometry | Lengths and breakout locations against drawing tolerances |
| Connector orientation | Housing orientation and cavity population against the drawing |
| Labels | Required part number, revision, and marking position |
| Protective materials | Sleeve or tape identification, coverage, and placement |
PPAP Submission
Where your customer requires a Production Part Approval Process (PPAP) submission, agree on the submission level before the build. PPAP assesses whether a production process can consistently meet specification requirements.
Compare the process failure mode and effects analysis (PFMEA) with the control plan to confirm each identified risk has a corresponding control. A missing-seal risk, for example, needs a defined seal-presence control and failure response. The part submission warrant (PSW) should reference that supporting package.
Final Inspection and Testing
We retain electrical records linked to each assembly and check circuit results against your schematic and acceptance limits. Require reports that identify test coverage and the test-program revision, along with any applicable high-potential (hipot) settings.
For sampled inspection, the agreed sampling plan should state the acceptance quality limit (AQL), lot size, and sample size. Define acceptance and rejection criteria, then decide the lot disposition. Our wire harness testing methods explain each test type in more depth.
Wire Harness Testers and Testing Equipment
A wire harness tester should demonstrate the required circuit coverage using your proposed test program. During a demonstration, introduce a known fault and check that the tester records the rejection.
Calibration records should cover the instrument used on the reported inspection date. Any outsourced report should identify the submitted samples so you can match results to your build. Evaluate wire harness testing equipment against these records:
| Equipment | Evidence to Request | Red Flag |
|---|---|---|
| Continuity and circuit-mapping tester | Approved pin map and test-program revision | Specified circuits omitted |
| Hipot or insulation-resistance tester | Required settings and calibration record | Settings lack specification references |
| Pull-force tester | Measured force against limits for the termination | Only a “pass” statement supplied |
| Crimp cross-section equipment | Identified sample images and agreed evaluation criteria | Images lack sample linkage |
Documentation and Traceability
Traceability matters most when you find a suspect material lot or a failed production setup and need to decide what to contain. Test record retrieval with a real shipment:
- Shipment identity: Match the delivered part number and revision with the shipment identifier.
- Production history: Retrieve the associated work order and inspection records for that delivery.
- Material linkage: Follow component-lot references to receiving records, then identify other shipments that share the suspect lot.
Shipment Records and Approved Deviations
A certificate of conformance should identify the supplied part and revision, with a shipment or lot reference linking it to your delivery. Compare it with the agreed inspection reports to spot unresolved nonconformances or approved concessions.
Our workmanship records document inspection results and defect disposition, including how we hold assemblies that fail inspection. For reworked parts, confirm the supplier repeated the checks before returning them to accepted stock.
Factory Audits and Third-Party Inspection
During an audit, compare a selected production record with the work instruction at the workstation. The auditor should also examine rejected-stock segregation and how operators get current instructions after a revision change.
Require the audit report to separate observed evidence from unverified statements, with an owner and closure requirement for each open finding.
Printable QC Scorecard
Print this scorecard and complete the final column during your supplier review. Enter verified, open, or unacceptable for each checkpoint, plus the supporting document or record number.
Supplier: ____________________
Factory: ____________________
Reviewer and Date: ____________________
Open Item: ____________________
Required Action: ____________________
Owner: ____________________ Due Date: ____________________
| Buyer Question | Required Evidence | Red Flag | Your Status and Supporting Record |
|---|---|---|---|
| Does certification cover this plant? | Verified certificate | Wrong site or expired coverage | |
| Which workmanship class applies? | Agreed on class and revision | Undefined acceptance criteria | |
| Do incoming parts match the approved BOM? | Receiving checks and material lots | Unapproved substitutions | |
| Can you verify termination controls? | Crimp height, pull-force, and required cross-sections | Checks without limits | |
| Does sample approval represent production? | FAI and required PPAP evidence | Unresolved approval conditions | |
| Can equipment verify required characteristics? | Coverage, results, and calibration | Required checks missing | |
| Which final checks cover this lot? | Visual/AQL plan and electrical reports | Undefined coverage | |
| Does the shipment declaration match delivery? | Certificate of conformance and lot reference | Missing revision or shipment linkage | |
| Can records identify affected shipments? | Material-to-shipment linkage | Containment scope unknown |
Discuss Your Wire Harness Requirements
At Cloom Tech, we manufacture customized wire harnesses and cable assemblies against every checkpoint above. We’re ISO 9001 and IATF 16949 certified and work to IPC/WHMA-A-620.
Our DFM feedback is based on your existing drawings, covering material selection, cost reduction, and production efficiency. We don’t offer product development, so your team approves every change. Samples take 3–4 weeks, and mass production takes 4–5 weeks. Send your drawings and required QC deliverables for a free quote.
Wire Harness Quality Control & Inspection FAQs
Is visual inspection enough for wire harness quality control?
No, visual inspection confirms visible assembly features, but it can’t show electrical resistance or dielectric performance. Combine the specified visual checks with electrical verification suited to the circuit requirements before you accept the finished harness.
What does electrical testing detect in a wire harness?
Depending on the test program, electrical testing finds open and shorted circuits, while resistance and insulation checks catch additional faults. Detection depends on the specified test coverage, so a continuity pass doesn’t prove the program assessed every possible defect.
Can a wire harness pass electrical testing but still fail later?
Yes, a harness can pass its electrical checks and later suffer damage from vibration or mechanical strain in service. Poor strain relief or abrasion can compromise a sound connection, so application validation must cover the operating environment as well as production conformity.
What is hipot testing, and why does it matter?
Hipot testing applies an elevated voltage to check dielectric withstand, which continuity testing can’t assess. Your approved specification should set test conditions that suit the assembly and its components.
Back to Top: Wire Harness Quality Control & Inspection: A Buyer’s Vetting Checklist